




DESIGNED TO REDUCE PRODUCT DEGRADATION
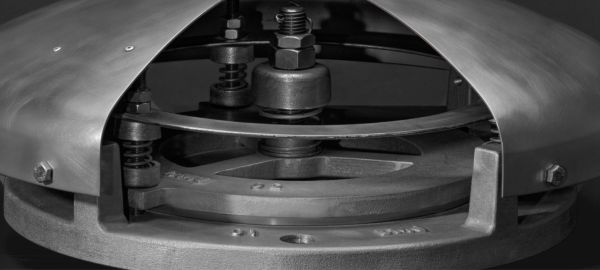
The GL body and rotor have been developed specifically for granular products.
We use cookies and other tracking technologies to improve your browsing experience on our website, to show you personalized content and targeted ads, to analyze our website traffic, and to understand where our visitors are coming from.


The GL rotary valve is designed for gravity feeding and pneumatic conveying of granular products. Its body and rotor configuration have been developed to minimise product degradation while retaining high pocket-filling efficiency. The inlet design further reduces product chopping, making the GL well-suited to applications where maintaining granule integrity is important.
The GL rotary valve is designed for gravity feeding and pneumatic conveying of granular products. Its body and rotor configuration have been developed to minimise product degradation while retaining high pocket-filling efficiency. The inlet design further reduces product chopping, making the GL well-suited to applications where maintaining granule integrity is important.
 Thank you
Your quote request has been received!
Something went wrong.
One moment..
GL DROP-THROUGH ROTARY VALVE
The GL combines a purpose-designed body and rotor with an inlet that minimises product chopping. The result is a rotary valve built around efficient pocket filling while reducing degradation as granular material passes through.
The GL body and rotor have been developed specifically for granular products.
Product protection is balanced with high filling efficiency.
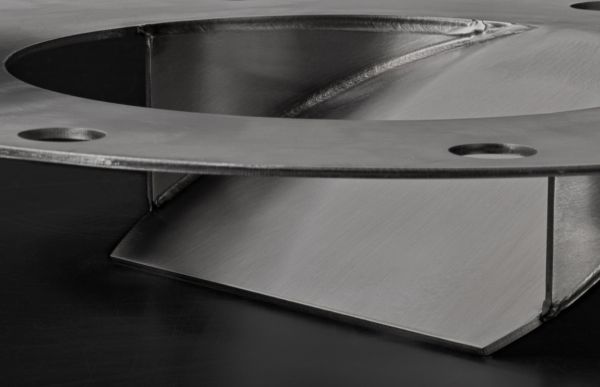
The inlet construction is shaped to reduce chopping as granular material enters the rotor pockets, providing additional protection for the product during handling.
GL DROP-THROUGH ROTARY VALVE
The GL body and rotor have been developed specifically for granular products. Their configuration helps minimise degradation as material passes through the valve.
Product protection is balanced with high filling efficiency. The rotor and body geometry are designed to retain the best possible pocket filling during gravity feeding and pneumatic conveying.
The inlet construction is shaped to reduce chopping as granular material enters the rotor pockets, providing additional protection for the product during handling.
Large air vent openings form part of the GL design and support its use in pneumatic conveying applications.
The GL is available in three housing configurations, which are an all-stainless-steel housing, a stainless-steel housing with aluminium end covers, or an anodised aluminium construction. Direct-drive and chain-drive options are available to suit different installation requirements.
ROTARY VALVE


The GL is available with an all-stainless-steel housing, a stainless-steel housing with aluminium end covers, or an anodised aluminium construction. The full end-disc rotor is 316 stainless steel. End covers use outrigged ball bearings, with gland packing used for shaft sealing.
Five sizes are available, ranging from 150 to 350, with capacities from 5 to 79 litres per revolution at 100% fill. Standard models handle product temperatures up to +150°C and a maximum pressure difference of 1.5 bar. Other options are available on request.


| GL Rotary Valve | 150 | 200 | 250 | 300 | 350 |
|---|---|---|---|---|---|
| LTR/REV AT 100% FILLING | 5 | 10 | 17.5 | 32 | 79 |
Technical modifications are possible, dimensions in mm.
*More detailed information is found in our product documentation
79
L/rev
Maximum listed capacity at 100% filling
5
sizes
Available from 150 to 350
+150°C
Maximum standard product temperature
1.5
Bar
Maximum standard pressure difference
Request a quote · 48h response
Thank you
Your quote request has been received!
Something went wrong.
One moment..


